Welcome to Zhengzhou Xinli Wear-Resistant Material Co. Ltd.
Welcome to Zhengzhou Xinli Wear-Resistant Material Co. Ltd.
With the growing adoption of smart home technology and increasing demand for high-end architectural decoration, the market for LED smart bathroom mirrors, anti-glare art mirrors, and customized decorative mirrors is expanding rapidly. However, during mirror sandblasting, downstream processors often face problems such as low backing-coating removal efficiency, glass edge chipping and breakage, uneven light transmission, excessively rough blasted surfaces, and iron contamination.
As a supplier of surface treatment and abrasive solutions, this article provides a systematic analysis of the key applications of mirror sandblasting—back-side coating removal for light transmission and front-side artistic frosting—covering abrasive material selection, grit-size matching, blasting pressure, and nozzle selection to help processors improve production efficiency and finished-product yield.
Mirror sandblasting is a surface treatment process that uses compressed air to propel abrasives such as Brown Fused Alumina, White Fused Alumina, or glass beads at high velocity onto the front or back surface of a mirror, thereby modifying its optical and surface characteristics.
Depending on the processing surface and desired result, mirror sandblasting can generally be divided into two major applications:
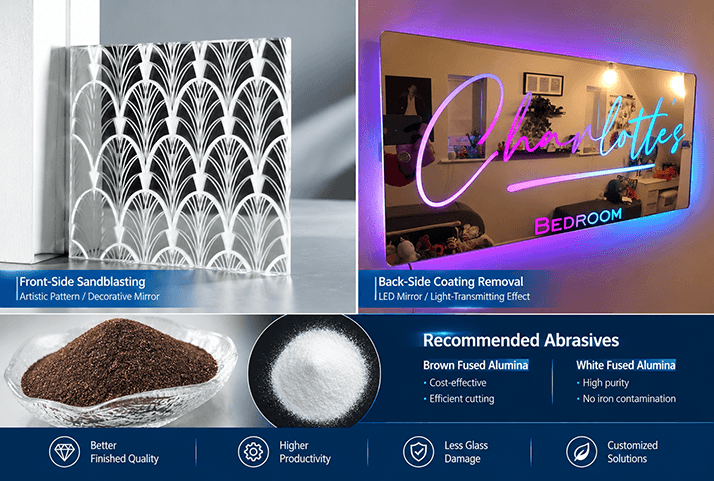
Process principle: Abrasive blasting is used to remove the silver resin paint layer and reflective silver layer from the back of the mirror, exposing the transparent glass substrate.
Main applications: This process is used to create light-transmitting areas such as LED light channels, touch-control icons, and display windows in smart bathroom mirrors. When LED strips are installed behind the mirror, light can pass through the blasted areas, creating a soft and uniform light-transmitting effect.
Process principle: A stencil or engraving film is used to protect the areas that do not require processing, while abrasive is directly blasted onto the front surface of the glass to create a microscopic roughened surface with diffuse reflection.
Main applications: This process can be used to create patterns, logos, anti-glare effects, and fingerprint-resistant matte surfaces with a refined tactile finish.
Different mirror sandblasting applications have significantly different requirements for abrasive hardness, purity, and cutting performance.
Characteristics: High aluminum oxide content (>99%), high hardness, strong cutting ability, good self-sharpening properties, and high cleanliness with minimal iron contamination.
Suitable applications: High-end LED smart mirror back-side coating removal and high-clarity front-side decorative frosting. Because it minimizes iron contamination and the risk of discoloration, it is a preferred abrasive for applications requiring high-quality light transmission and a clean, uniform matte surface.
Characteristics: Cost-effective, relatively high toughness, and efficient cutting performance.
Suitable applications: Rapid removal of silver paint and primer from the back of conventional mirrors in applications where cost efficiency is important. For high-end mirror processing, attention should be paid to the potential impact of trace impurities.
To help process engineers match production parameters more precisely, the following table summarizes key recommended parameters for mirror sandblasting applications:
| Processing Requirement | Recommended Abrasive | Recommended Grit Size | Recommended Blasting Pressure | Recommended Nozzle | Target Result |
|---|---|---|---|---|---|
| LED mirror back-side coating removal and light transmission | White Fused Alumina / Brown Fused Alumina | 120#–180# (150# recommended) | 0.30–0.45 MPa (not recommended to exceed 0.5 MPa) | Boron Carbide nozzle 6.0–8.0 mm | Rapid removal of paint and reflective layers with smooth edges and reduced glass damage. |
| Ultra-fine matte / anti-glare front-side finishing | High-purity White Fused Alumina | 220#–280# | 0.20–0.35 MPa | Boron Carbide / Silicon Carbide nozzle 4.0–6.0 mm | Fine and uniform matte surface with good diffuse reflection. |
| Front-side artistic pattern engraving | White Fused Alumina | 150#–200# | 0.25–0.40 MPa | Boron Carbide nozzle 6.0–8.0 mm | Clear patterns with consistent surface haze and good masking protection. |
Mirrors are brittle materials. Excessive pressure (>0.5 MPa) can easily cause microcracks or edge chipping in the glass, while insufficient pressure (<0.2 MPa) may not effectively remove highly adherent backing paint.
A stable blasting pressure of approximately 0.3–0.4 MPa is recommended, with the spray gun maintained at an angle of 45°–60° to the mirror surface. This helps avoid stress concentration caused by direct 90° perpendicular impact.
Material recommendation: Mirror sandblasting is commonly performed using dry blasting or high-pressure wet blasting, and abrasive particles can cause significant nozzle wear. Boron Carbide (B₄C) nozzles are strongly recommended for their excellent wear resistance. Their service life can be approximately 3–5 times that of carbide nozzles, helping maintain a stable abrasive flow over extended operation.
Nozzle diameter and design: For large-area LED light-channel coating removal, Venturi nozzles are recommended because they provide a wider spray pattern and more uniform impact.
For small localized touch-control icons or fine patterns, straight-bore micro nozzles are recommended.
When the nozzle orifice has worn and increased by more than 15%, it should be replaced promptly. Otherwise, the resulting changes in air pressure and abrasive flow can lead to uneven blasting.
Abrasives used in a circulating blasting system gradually fracture into smaller particles as a result of repeated impact.
If excessive dust and fine particles accumulate, light transmission may decrease or the surface texture may become inconsistent.
An air-classification and abrasive-recovery system is therefore recommended to remove excessively fine and ineffective particles in a timely manner and replenish fresh abrasive to maintain a consistent particle-size distribution.
As a professional abrasive supplier, we are committed to providing White Fused Alumina, Brown Fused Alumina, and customized abrasive grades for glass processing and surface treatment applications.
For samples or a customized abrasive and sandblasting process optimization solution, please contact our technical team.
 English
 Русский
 日本語
 한국어
 Español
 Tiếng Việt
 Deutsch
 Français
 Italiano
 Português